CNC4Newbie
CNC4Newbie Upshot Mill
Rack-and-pinion CNC kit with non-GRBL electronics packages, five kit sizes
Use with Easel Pro →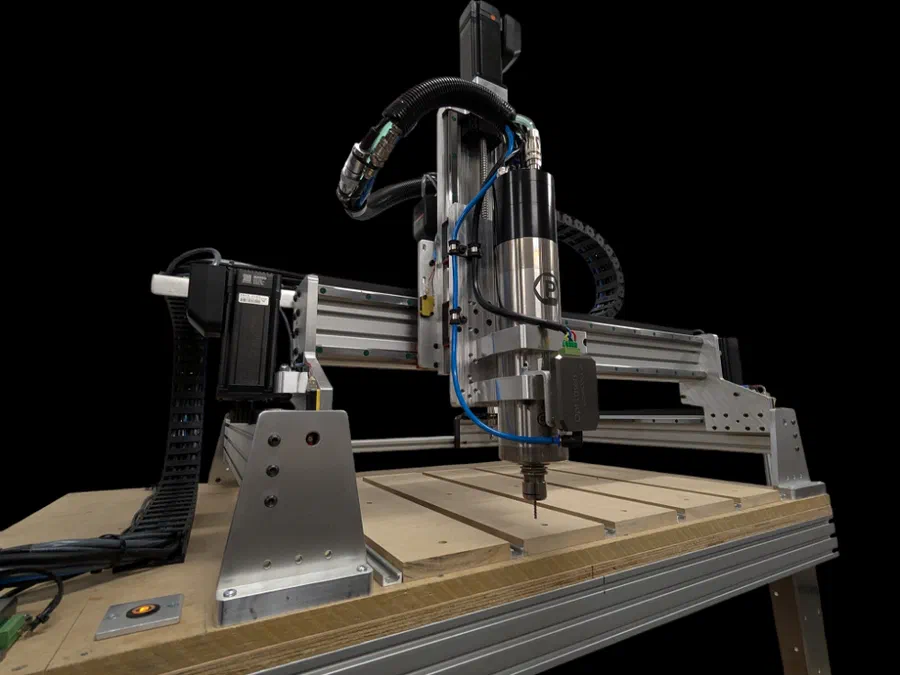
About the Machine
The Upshot Mill covers multiple kit sizes on one product page (2424, 4824, 4836, 4848, and 4896 in Easel’s menu; CNC4Newbie’s page also lists a 3636 size not in Easel’s menu). CNC4Newbie states a work area up to 50 x 98 in (max 68 x 110 in footprint, 8in clearance below the gantry) but does not publish a per-size breakdown table. It runs rack-and-pinion drive on X/Y and an HD ballscrew-driven Z axis with 8in of travel, 15mm square linear bearings on every axis, and can take a round- or square-body spindle up to 2.2kW, not included; mount options run from 65mm up to 89mm.
Cut Settings on this Machine
Every cut starts with one formula: Feed Rate = Spindle Speed (RPM) x Chip Load x Number of Cutting Edges (flutes). Chip load is the thickness of material each cutting edge removes in one revolution of the bit. This number comes from the manufacturer of the bit, which publishes a chip-load chart for each bit diameter and material. Look up your exact bit and material, start from the middle of the published range, and you have the third number in the formula. The chart below shows the recommended spindle speed for each material and bit type.
| Material | Solid carbide bit (RPM) | HSS & carbide-tipped bit (RPM) |
|---|---|---|
| Plastic (hard & soft) | 18,000 | 8,000 |
| Soft woods (MDF, particleboard, etc.) | 22,000 | 10,000 |
| Hard wood (oak, maple, etc.) | 16,000 | 7,000 |
| Aluminum | 12,000-14,000 | 5,500 |
| Aluminum, softer grades (such as 3003) | 10,000 | 5,000 |
| Foam (harder foams; soft foams do not rout well) | 18,000 | 8,000 |
| Composites | 12,000 | 5,000 |
If this machine's spindle cannot reach the listed speed, run the spindle at its maximum and control the cut with feed rate. For 65mm trim routers, the DeWalt DW611 dial maps to: 1 = 16,000; 2 = 18,200; 3 = 20,400; 4 = 22,600; 5 = 24,800; 6 = 27,000 RPM.
The Upshot Mill ships without a spindle, so its top RPM depends on whatever unit you mount, up to 2.2kW, check that unit’s own rating plate against the chart rather than assuming a number. Its rack-and-pinion X/Y drive, HD ballscrew-driven Z axis with 8in of travel, and 15mm square linear bearings on every axis are built for real rigidity. A truly rigid machine with a powerful spindle can cut as deep as the bit is wide in a single pass, but that takes real spindle torque, a drive train and clamps that hold firm, a gantry that will not flex, and enough mass to soak up vibration. With a suitable spindle mounted, the Upshot Mill can handle solid depth per pass, but still build up gradually. Push too deep and the bit deflects and chatters, leaving scalloped edges, or it rubs instead of cutting and burns the material. The fastest way to dial in a cut is to see what has already worked for other people.
Worked example for feed rate: 1/8in (3.175mm) two-flute solid carbide end mill in hard wood. The chart says 16,000 RPM. With the bit maker’s 0.025mm per tooth (0.0010 in): 16,000 x 0.025 x 2 = 800 mm/min (31 in/min) feed. For depth per pass, start shallow and check Community Cut Settings in Easel for what works on the CNC4Newbie Upshot Mill. If the cut sounds strained, reduce the depth, not the feed. Slowing the feed below the chip load makes the bit rub instead of cut.
Community Cut Settings shows the spindle speed, feed rate, and depth per pass other makers actually run for your machine, material, and bit.
CNC has never been easier
Using this machine with Easel
The Upshot Mill’s electronics packages run either a C4N Controller with UC100/UCcnc software or a Masso G3 Touch, and neither is GRBL or FluidNC, so Easel’s live Driver and Rapid Connect do not drive this machine directly. Instead, set up a Non-GRBL Machine Profile for the Upshot Mill in Easel, design your project as usual, then use Project > Download G-code to save an .nc file. If you have the UC100/UCcnc package, open that .nc file in the UCCNC software on the PC wired to the mill and run it from there. If you have the Masso G3 Touch package, transfer the .nc file to the controller over its built-in WiFi via Masso Link, or by USB drive, and run it from the touchscreen. Either way, Easel handles design and toolpath generation, and the controller’s own software runs the job.
Try Easel Free →Start creating with your CNC
Create your free Easel account and connect your machine in minutes.
Easel Free Trial →