Lunyee
Lunyee 4040 Pro
Compact CNC router with a 100W spindle and a ball-screw Z-axis
Use with Easel Pro →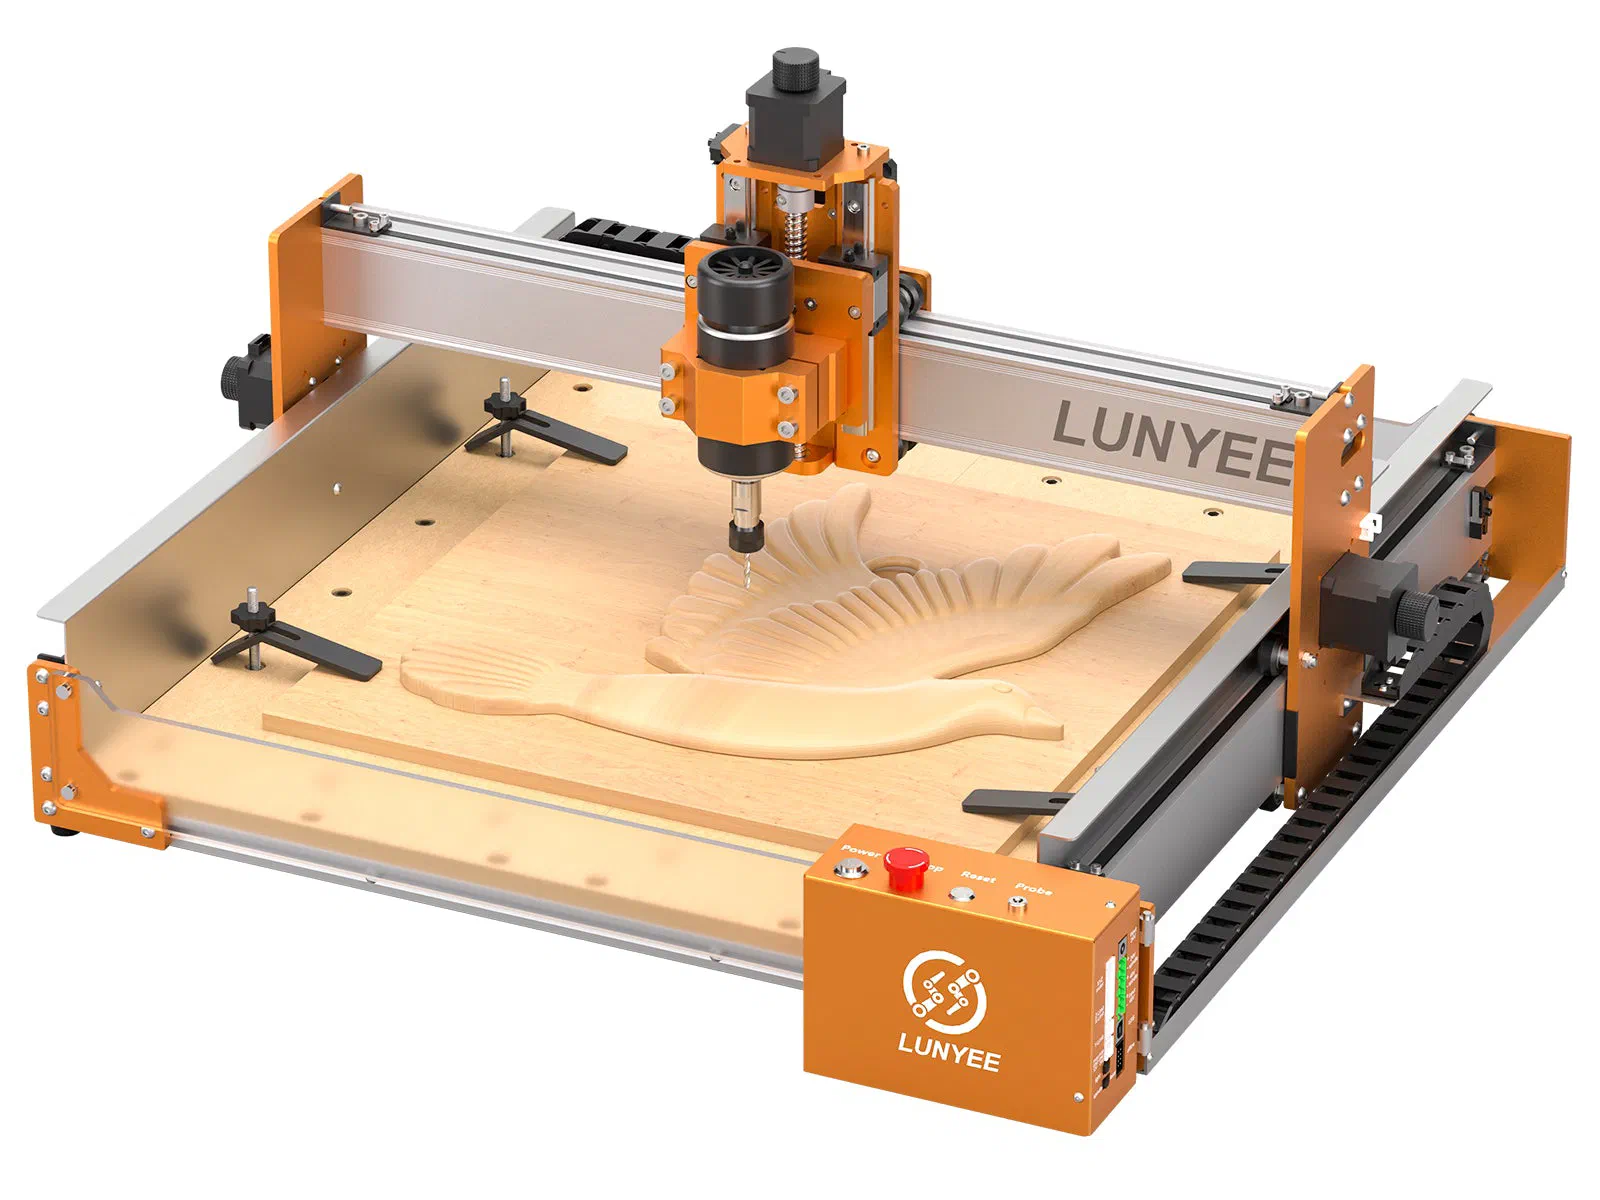
About the Machine
The 4040 Pro is a compact all-metal CNC router with a 400 x 400 x 90 mm working area, a 100W spindle (0 to 10,000 RPM), and Nema 17 stepper motors (1.68 A, 0.55 Nm torque). Its Z-axis rides on dual HG15 linear guides with a 1204 ball screw.
Cut Settings on this Machine
Every cut starts with one formula: Feed Rate = Spindle Speed (RPM) x Chip Load x Number of Cutting Edges (flutes). Chip load is the thickness of material each cutting edge removes in one revolution of the bit. This number comes from the manufacturer of the bit, which publishes a chip-load chart for each bit diameter and material. Look up your exact bit and material, start from the middle of the published range, and you have the third number in the formula. The chart below shows the recommended spindle speed for each material and bit type.
| Material | Solid carbide bit (RPM) | HSS & carbide-tipped bit (RPM) |
|---|---|---|
| Plastic (hard & soft) | 18,000 | 8,000 |
| Soft woods (MDF, particleboard, etc.) | 22,000 | 10,000 |
| Hard wood (oak, maple, etc.) | 16,000 | 7,000 |
| Aluminum | 12,000-14,000 | 5,500 |
| Aluminum, softer grades (such as 3003) | 10,000 | 5,000 |
| Foam (harder foams; soft foams do not rout well) | 18,000 | 8,000 |
| Composites | 12,000 | 5,000 |
If this machine's spindle cannot reach the listed speed, run the spindle at its maximum and control the cut with feed rate. For 65mm trim routers, the DeWalt DW611 dial maps to: 1 = 16,000; 2 = 18,200; 3 = 20,400; 4 = 22,600; 5 = 24,800; 6 = 27,000 RPM.
The 4040 Pro’s 100W spindle tops out at 10,000 RPM, below most of the chart, and it has the least power of Lunyee’s router lineup. A small spindle like this loses torque fast under load, so leave it near its top speed for everything and control the cut with feed rate. Depth per pass is where the machine itself matters. A truly rigid machine with a powerful spindle can cut as deep as the bit is wide in a single pass, but that takes real spindle torque, a drive train and clamps that hold firm, a gantry that will not flex, and enough mass to soak up vibration. This machine falls well short of that bar, so keep passes shallow: push too deep and the bit deflects and chatters, leaving scalloped edges, or it rubs instead of cutting and burns the material. The fastest way to dial in a cut is to see what has already worked for other people.
Worked example for feed rate: 1/8in (3.175mm) two-flute solid carbide end mill in hard wood. The chart says 16,000 RPM. With the bit maker’s 0.025mm per tooth (0.0010 in): 16,000 x 0.025 x 2 = 800 mm/min (31 in/min) feed. For depth per pass, start shallow and check Community Cut Settings in Easel for what works on the Lunyee 4040 Pro. If the cut sounds strained, reduce the depth, not the feed. Slowing the feed below the chip load makes the bit rub instead of cut.
Community Cut Settings shows the spindle speed, feed rate, and depth per pass other makers actually run for your machine, material, and bit.
CNC has never been easier
Using this machine with Easel
The 4040 Pro runs GRBL 1.1f on its 32-bit ARM control board, so it connects directly to Easel. Install the free Easel Driver and plug in over USB, or connect driverless with Rapid Connect in a Chromium browser (Chrome, Edge, or Opera). Design in the browser, then the Carve button homes, zeroes, and runs the job with live progress. You can also export G-code to run from another sender. Select 4040 Pro CNC in Easel’s machine menu to size the canvas.
Prefer not to install anything? Rapid Connect lets any GRBL machine, this one included, connect straight from your browser. If you go the driver route, grab it from the downloads page and follow the step-by-step install guide.
Try Easel Free →Start creating with your CNC
Create your free Easel account and connect your machine in minutes.
Easel Free Trial →