Onefinity
Onefinity Elite Series (Gen 2)
Large-format CNC in three cut areas with a closed-loop Redline RTS-2 controller
Use with Easel Pro →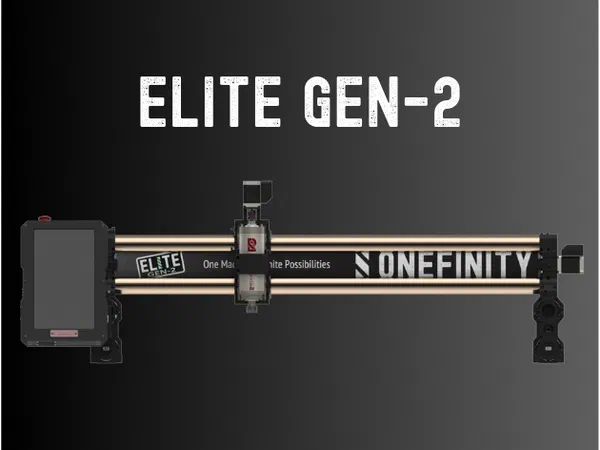
About the Machine
The Onefinity Elite Series (Gen 2) is Onefinity’s newest large-format CNC, introduced in November 2025 and sold in three cut areas from one product page: Woodworker at 33in x 33in, Journeyman at 49in x 33in, and Foreman at 49in x 49.125in. It drives X and Y on a 1616 ball screw (16mm per revolution) and Z on a 1610 ball screw (10mm per revolution), with closed-loop 2 Nm stepper motors on X and Y and a 1.2 Nm braking stepper on Z, on 60mm hardened-steel linear shafts on X. No router or spindle ships with the machine: it’s built for an optional Redline spindle in a 65mm or 80mm mount.
Cut Settings on this Machine
Every cut starts with one formula: Feed Rate = Spindle Speed (RPM) x Chip Load x Number of Cutting Edges (flutes). Chip load is the thickness of material each cutting edge removes in one revolution of the bit. This number comes from the manufacturer of the bit, which publishes a chip-load chart for each bit diameter and material. Look up your exact bit and material, start from the middle of the published range, and you have the third number in the formula. The chart below shows the recommended spindle speed for each material and bit type.
| Material | Solid carbide bit (RPM) | HSS & carbide-tipped bit (RPM) |
|---|---|---|
| Plastic (hard & soft) | 18,000 | 8,000 |
| Soft woods (MDF, particleboard, etc.) | 22,000 | 10,000 |
| Hard wood (oak, maple, etc.) | 16,000 | 7,000 |
| Aluminum | 12,000-14,000 | 5,500 |
| Aluminum, softer grades (such as 3003) | 10,000 | 5,000 |
| Foam (harder foams; soft foams do not rout well) | 18,000 | 8,000 |
| Composites | 12,000 | 5,000 |
If this machine's spindle cannot reach the listed speed, run the spindle at its maximum and control the cut with feed rate. For 65mm trim routers, the DeWalt DW611 dial maps to: 1 = 16,000; 2 = 18,200; 3 = 20,400; 4 = 22,600; 5 = 24,800; 6 = 27,000 RPM.
The Elite Series (Gen 2) doesn’t ship with a spindle of its own: it’s built around Onefinity’s optional Redline spindle, so check that unit’s plate for its actual RPM range before you dial in a cut. What the frame itself brings is real rigidity: closed-loop 2 Nm steppers on X/Y, a 1.2 Nm braking stepper on Z, 1616/1610 ball screws under full snap-in covers, and a 60mm hardened-steel X shaft. A truly rigid machine with a powerful spindle can cut as deep as the bit is wide in a single pass, but that takes real spindle torque, a drive train and clamps that hold firm, a gantry that will not flex, and enough mass to soak up vibration. Gen 2’s heavier frame and stronger steppers get you most of the way there mechanically, so once you know your spindle’s actual power and RPM you can push depth per pass further than on a lighter hobby machine. Push too deep for the bit and spindle you have and it will still deflect and chatter, leaving scalloped edges, or rub instead of cutting and burn the material. The fastest way to dial in a cut is to see what has already worked for other people.
Worked example for feed rate: 1/8in (3.175mm) two-flute solid carbide end mill in hard wood. The chart says 16,000 RPM. With the bit maker’s 0.025mm per tooth (0.0010 in): 16,000 x 0.025 x 2 = 800 mm/min (31 in/min) feed. For depth per pass, start shallow and check Community Cut Settings in Easel for what works on the Onefinity Elite Series (Gen 2). If the cut sounds strained, reduce the depth, not the feed. Slowing the feed below the chip load makes the bit rub instead of cut.
Community Cut Settings shows the spindle speed, feed rate, and depth per pass other makers actually run for your machine, material, and bit.
CNC has never been easier
Using this machine with Easel
The Onefinity Elite Series (Gen 2) runs the Redline Control System on a Realtime CNC RTS-2 closed-loop motion controller, which is not GRBL or FluidNC, so Easel’s live Driver and Rapid Connect do not drive it directly. Instead, set up a Non-GRBL Machine Profile for this machine in Easel, design your project as usual, then use Project > Download G-code to save an .nc file. Load that file onto the controller over USB, or transfer it to the machine’s standalone Redline HMI touchscreen using its WiFi or Ethernet connection, and run the job from the HMI.
Try Easel Free →Start creating with your CNC
Create your free Easel account and connect your machine in minutes.
Easel Free Trial →